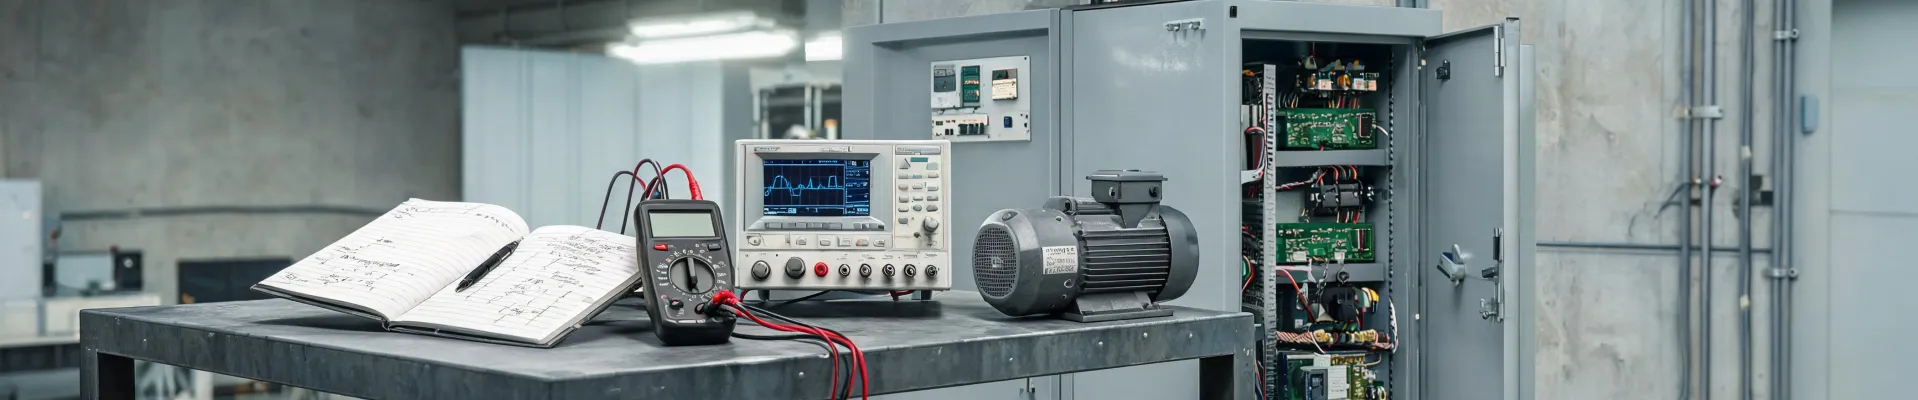
That February Morning in Receiving
I’m the quality and brand compliance manager at Extech Multimeter. I review every tester batch before it reaches customers—roughly 300 units a month. In 2024, I rejected 17% of first deliveries due to missing calibration documents, CAT rating mismatches, or labeling issues. That number still bothers me.
In February 2024, we needed 500 clamp meters, 300 multimeters, and 1,200 bulk sensors for a utility contractor order. Our usual channel quoted $42,800. A new tester supplier quoted $38,000—about 11% lower. Purchasing loved it. The numbers said save $4,800. My gut said slow down.
We ordered 200 clamp meters as a pilot. That felt like a reasonable compromise. Then the pallet arrived.
What the First Inspection Showed
We inspect every incoming batch: visual checks, functional tests, and a full documentation review. The clamp meter jaws had flashing. That’s cosmetic—annoying, but not a dealbreaker. The bigger issue was the label. It said CAT III 600V, but the manual didn’t reference IEC 61010-2-032. The calibration certificates were factory certificates without NIST traceability. The bulk sensors had no serial-to-lot traceability.
We pulled 10 clamp meters and tested them against a known reference. Readings varied by 8–12% on a 10 A load. For field service, that isn’t a rounding error. It’s a reliability problem. We sent three units to an external lab. They found fuses that weren’t rated for the marked CAT III environment. That’s a compliance failure, not a cosmetic one.
Why is that fuse detail so important? Because CAT ratings describe where a meter can safely be used. CAT III covers distribution-level circuits. CAT IV covers the origin of the installation. If the fuse and input protection don’t match the label, the meter may not protect the technician when a transient hits. That’s not a spec sheet problem. That’s a safety problem.
The Vendor’s Response and My Second-Guessing
The vendor claimed it was within industry standard.
I rejected the batch. Then I second-guessed myself. Had I been too strict? We were under deadline. Maybe we could have sorted the worst units and shipped the rest. For two weeks, I kept wondering if we’d just made the project harder for no reason.
Then the lab report came back. The fuse issue confirmed the rejection. If those clamp meters had gone to a utility crew, a transient could have injured someone or destroyed the meter. That’s when I stopped treating compliance paperwork as paperwork.
The Number That Changed How I Buy
We air-freighted replacements from our approved tester supplier. The original $4,800 savings turned into:
- Air freight: $2,100
- Re-testing and sorting: $1,800
- Expedited production: $3,200
- Overtime and admin: $900
Total: about $8,000 over budget, plus a 6-day delay to the contractor. When I compared the two invoices side by side, I finally understood why the lowest quote is rarely the lowest cost. It took me four years and 200+ supplier reviews to understand that a tester supplier’s value is in documentation and consistency, not just the quote.
As of January 2025, I still verify every standard because IEC and UL requirements can update. This was accurate for our process at that time. I’d rather spend two days checking than two weeks fixing a field failure.
What Clamp Meter Compliance Requirements Actually Include
For our Extech Multimeter orders—including the Extech multimeter 410 and clamp meter batches—we now require a compliance packet. It’s not just a CE mark.
Core requirements we check
- IEC 61010-1 general safety, plus IEC 61010-2-032 for handheld current clamps.
- CAT rating marked on the instrument: CAT III or CAT IV as applicable. The manual must explain the measurement category.
- NIST-traceable calibration with as-found and as-left data, not just a generic certificate.
- Fuse and input protection rated for the CAT environment. This is where cheap units often cut corners.
- Serial number traceability for bulk sensors and clamp meters, so a batch issue can be isolated.
- RoHS and REACH declarations and consistent labeling.
I’m not 100% sure why some suppliers treat calibration certificates as optional. My best guess is they assume buyers won’t check. But in B2B electrical work, one unchecked batch can become a field failure.
To be fair, not every low-cost supplier is bad. Some are excellent. But the ones that can’t provide traceable evidence usually aren’t saving you money—they’re transferring risk to you.
How We Source Extech Multimeters and Bulk Sensors Now
We use a simple TCO model: unit price + compliance verification + failure risk + delay cost. It changed our vendor scorecard. Unit price is 30% of the score, not 70%. Quality history, documentation, and responsiveness make up the rest.
For bulk sensor orders, we require samples from the production run—not golden samples. For Extech multimeter and clamp meter batches, we audit the compliance file before shipping. That process added about two days upfront. But it has cut our rejection rate from 17% to under 4% in 2024. The upfront work pays for itself.
Why does this matter? Because a tester supplier is not just selling a box. They’re selling the confidence that the number on the display matches reality. When a technician uses an Extech multimeter or clamp meter, they’re making decisions that affect safety, downtime, and customer trust.
The Lesson I Keep Relearning
Low price isn’t the problem. Missing evidence is. A tester supplier can be inexpensive and still be good—if they can prove the CAT rating, calibration, and fuse protection. But when the price is the only thing that looks good, the hidden cost is already in the box.
Now when someone says we can save $4,800, I ask: What does the calibration certificate say, and who signed it? That question has saved us more than once. And it’s why our Extech Multimeter process is strict. Not because we like paperwork, but because the person holding the meter deserves a tool that does what the label says.
Elaine Zhou
Elaine Zhou is a cable-management and connectivity analyst specializing in cable trays, cable glands, ties, conductors, terminations, plugs, sockets, and outlet connections. She applies IEC 61537 tray tests, IEC 62444 gland requirements, and IEC 60364-5-52 wiring criteria while examining safe current capacity, voltage drop, bend radius, segregation, grounding, sealing range, and enclosure entry. She helps contractors and engineers choose coordinated routes and connections for environmental exposure, expansion capacity, installation labor, reliability, and maintenance access.